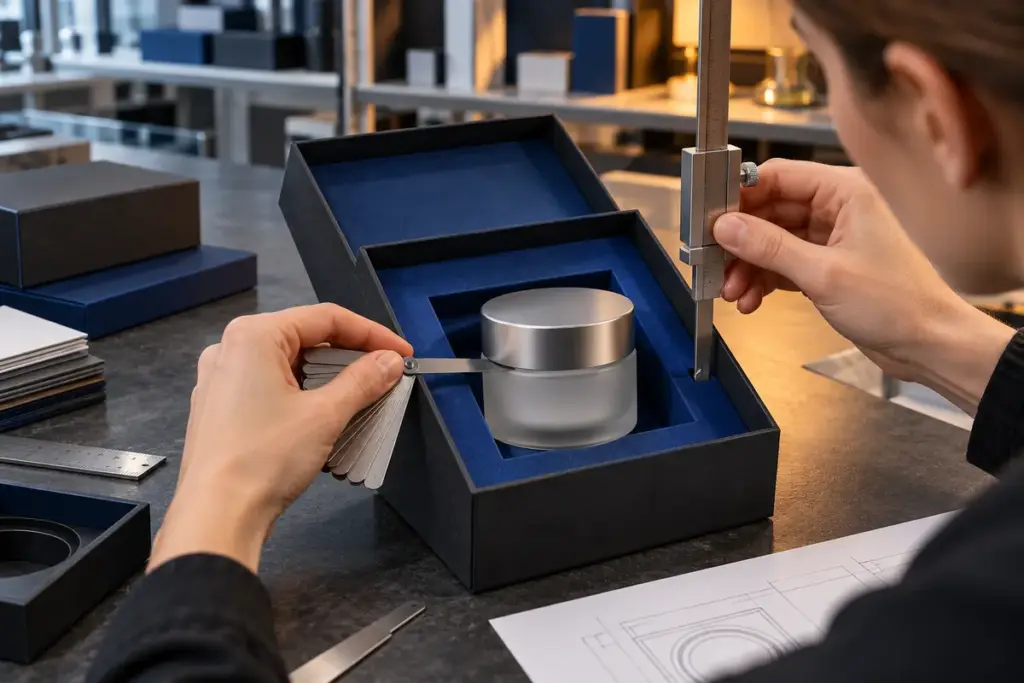
Складная коробка defect looks simple on the packing line and complicated on a claim form. The buyer sees a cracked crease or a seam that opened; the factory needs to know where it started before it can fix the run. This article explains what the common folding carton defects look like, where they may originate, and what evidence you should record so a conversation with a supplier rests on facts. It focuses on the physical carton and the complaint, not on choosing a supplier or on building a full quality system.
Which Folding Carton Defects Affect Function or Appearance?
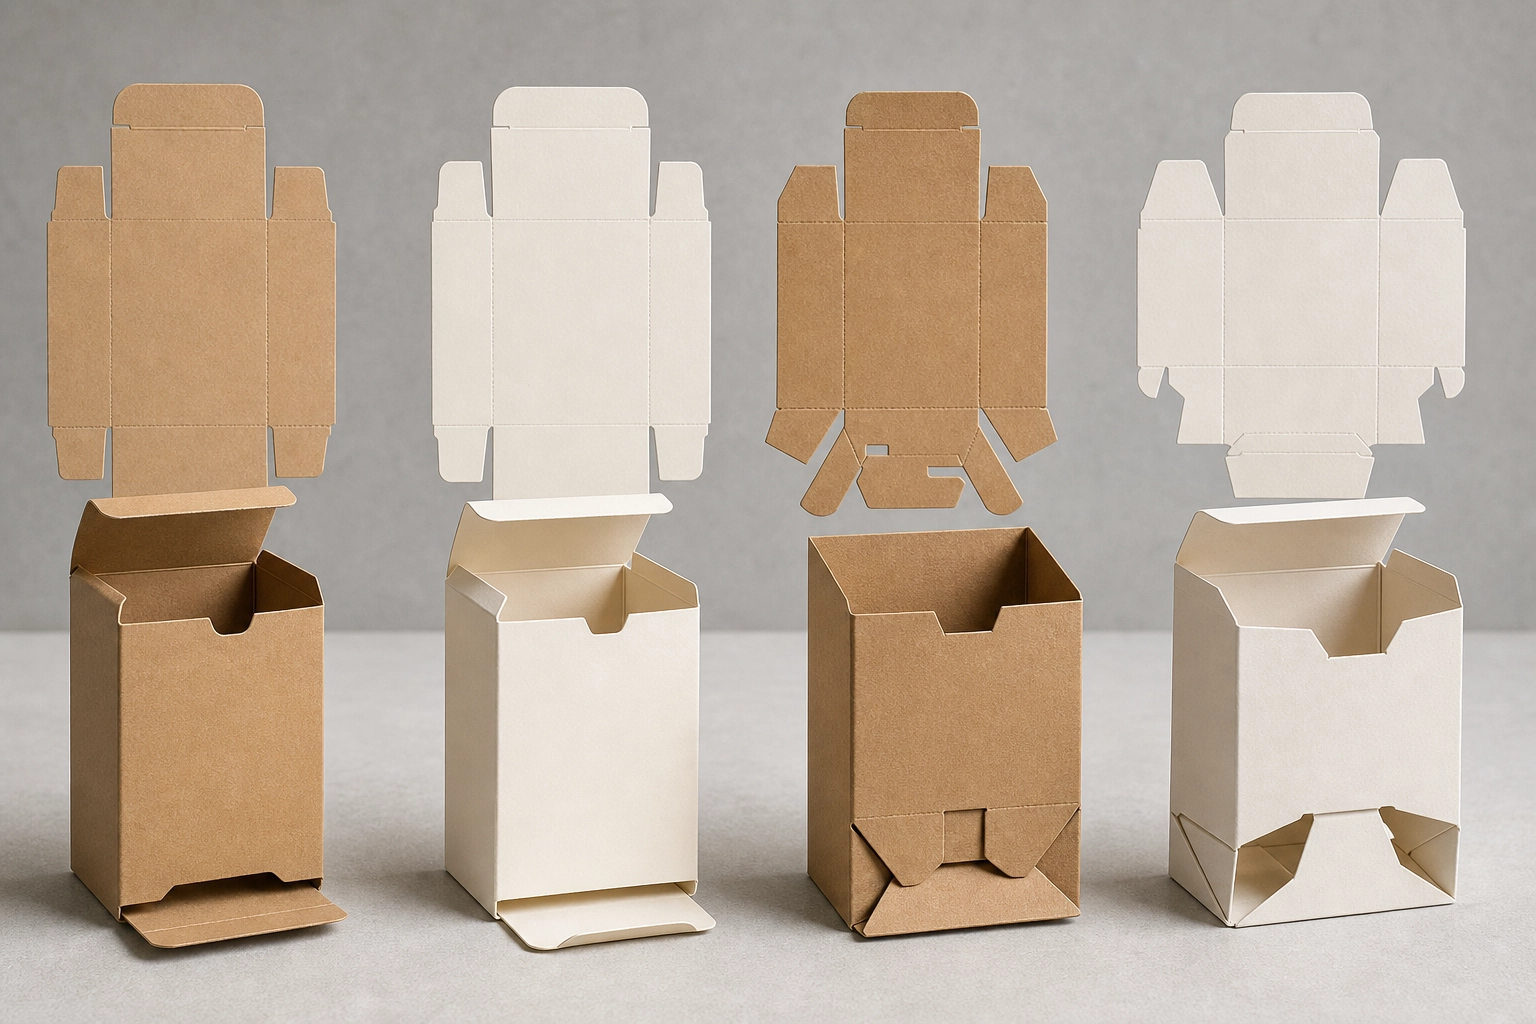
Defects can affect function, появление, or both, and the severity determines how urgently each one must be handled. A functional defect prevents the carton from being formed, closed, filled, or protected as intended. A cosmetic defect changes its appearance without necessarily stopping use. Crease cracking, lamination lifting, and print damage can fall into either group depending on their extent and location. The table below maps the common folding carton defects to where they show up.
| Defect Group | Typical Signs | Impact |
|---|---|---|
| Crease and board | Cracking along the fold, spring-back | Cosmetic or functional, depending on severity |
| Die-cut and fit | Misalignment, size variation, tabs out of place | Functional |
| Glue and squareness | Open seam, excess glue, out-of-square box | Functional |
| Print and finish | Color shift, misregistration, lifting, foil shift, scuff | Usually cosmetic; may affect function or readability |
Keep the groups separate when you report a problem, because a cosmetic variance and a functional failure often carry different acceptance limits on the same order. A defect that fails a closure does not belong in the same bucket as a faint scuff on a display panel. Your reference for any judgment is the approved sample and the drawing, not a general idea of what a good carton looks like.
Why Do Folding Cartons Crack Along the Crease?
Crease cracking shows as a split or a pale line along the fold, sometimes with the surface coating breaking open. Several sources can produce the same mark, and a photo alone rarely tells you which one applies. The scoring may be too shallow or too deep for the board. The grain orientation may not suit the primary fold lines. The board may be dry, or a coating or laminate may be brittle at that radius.
Do not treat cracking as proof of one cause. It can originate in the board condition, grain orientation, crease rule and matrix, applied pressure, or a coating or laminate over the fold. A crease that is too shallow or too wide can resist folding, while excessive pressure or an incorrectly matched rule and matrix can damage the board. Confirm the cause against the approved sample, board specification, and converting setup.
Board construction sits behind many of these causes. Fiber composition, ply structure, moisture condition, жесткость, surface coating, and lamination can all change how a board behaves at the fold. Two boards with the same caliper may therefore require different creasing settings. When reporting a crack, record the exact board grade, caliper, покрытие, ламинирование, and storage condition so the manufacturer can evaluate the material and crease setup together.
What Causes Poor Creasing and Difficult Assembly?
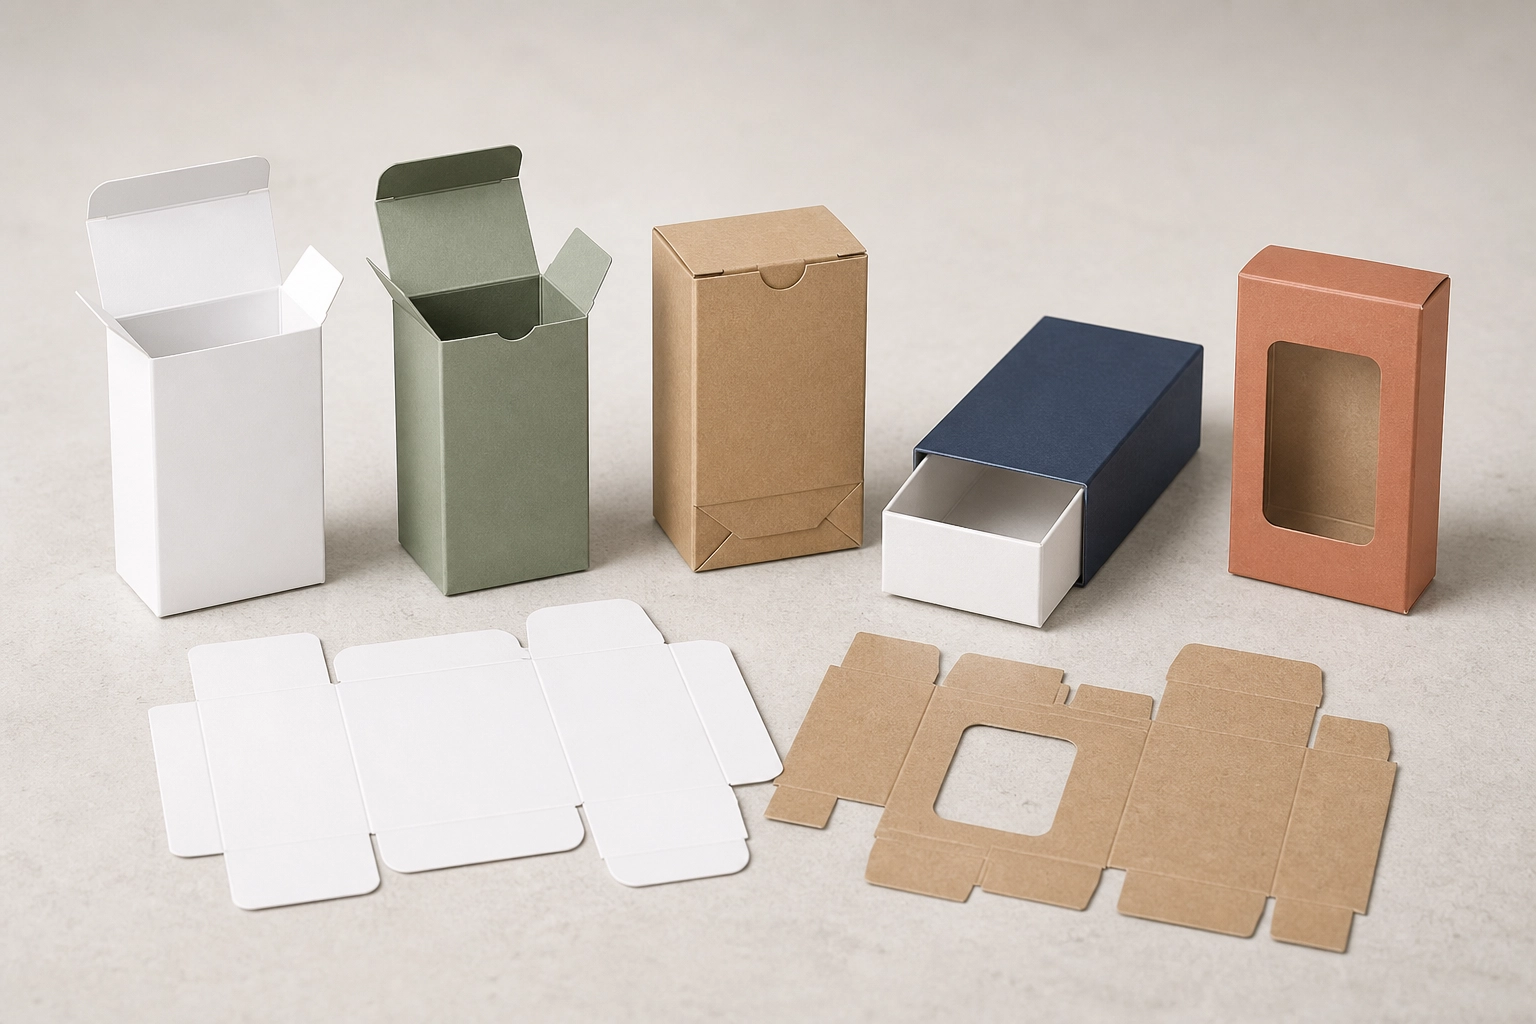
Poor creasing reveals itself during assembly. The carton fights the operator, springs back instead of holding a sharp fold, or sits crooked once formed. A crease that is inconsistent across the run makes an automatic folder-gluer jam, and it makes hand assembly slow and uneven.
The likely factors sit in the crease depth, the scoring rule matched to board caliper, and the grain direction. Each interacts with the others, so a fix to one dimension may shift the result. There is no universal crease width to cite, because the right value tracks the specific board grade and caliper you ordered. Confirm the crease against the approved sample and state the board you used when you report the problem.
Assembly tooling and method change the picture too. A carton folded by hand tolerates a slightly stiff crease that an automatic folder-gluer will not, so tell the supplier how the boxes will be erected on your line. If a set arrives hard to open or slow to square, note whether the difficulty appears at one station or across the batch. That pattern points the diagnosis toward setup rather than material.
Why Do Die-Cut Cartons Have Fit or Alignment Problems?
Die-cut defects change the geometry of the flat blank before it is ever folded. Look for cut and crease lines that sit off their intended position, or tabs that do not line up with the seams they close. Also check for blanks that vary in size from one end of the run to the other. A small dimensional drift in the blank becomes a visible gap or a misaligned closure on the finished carton.
Possible sources include a worn or mis-set die, registration drift on the cutting press, or board that moves with humidity. None of these is a confirmed root cause on sight. When you report an alignment problem, attach a measurement against the drawing. Note where in the run the off-size blanks appeared, so the factory can separate a die issue from a setup issue.
Grain orientation and humidity also affect dimensional stability and folding behavior. Board can change dimensions as it gains or loses moisture, while a grain orientation that does not suit the primary fold lines may increase folding resistance. Record the specified grain direction and the storage conditions before concluding that the cutting die caused the misfit.
Found Folding Carton Defects in a Sample or Shipment?
What Causes Glue Failure or an Out-of-Square Carton?
A glue seam that opens or a carton that stands out of square can stop the package from working. Do not assume that every open seam means the adhesive itself is defective. Possible causes include an incorrect glue amount or position, dust or coating on the glue tab, poor surface compatibility, insufficient compression or setting time, and a seam gap created by cutting or folding variation.
An out-of-square carton may come from the relationship between the cut, складка, folding setup, and glue tab rather than from the adhesive alone. Record whether the problem affects every unit or appears intermittently, and inspect the failed seam. Note whether the adhesive remains on one surface, transfers to both surfaces, or is missing from part of the tab. These observations help the manufacturer narrow the cause without treating the first assumption as proof.
How Do Printing and Finishing Defects Appear?
Print and finishing defects are mostly cosmetic, which means they test your acceptance limits more than your carton’s function. Color variation shows when a run drifts from the approved standard or when a reprint does not match the original. Misregistration puts one ink plate slightly off, softening edges or showing a sliver of white. Lamination can lift at an edge, foil can shift by a fraction of a millimeter, and a scuff can mark a dried ink surface during handling.
Because acceptable appearance varies by panel and application, the approved print reference and agreed inspection method matter. ИСО 12647-2:2013 provides process-control parameters for offset lithographic printing, but it does not replace a carton-specific agreement covering board, покрытие, фольга, ламинирование, and visible acceptance limits. Judge the finished carton against the signed sample and the agreed specification rather than applying one number to every material and finish. PK Paper Box’s color matching guide explains how a reproducible reference can be established.
Handle each finding against the run record, not a single unit. A color that reads off on one carton from the end of a long run is a different report from a color that reads off across the whole batch. Save the position in the run where the change appeared, and pair it with the approved standard, so the supplier can tell press drift from a proof that never matched.
How Should Buyers Document and Report Defects?
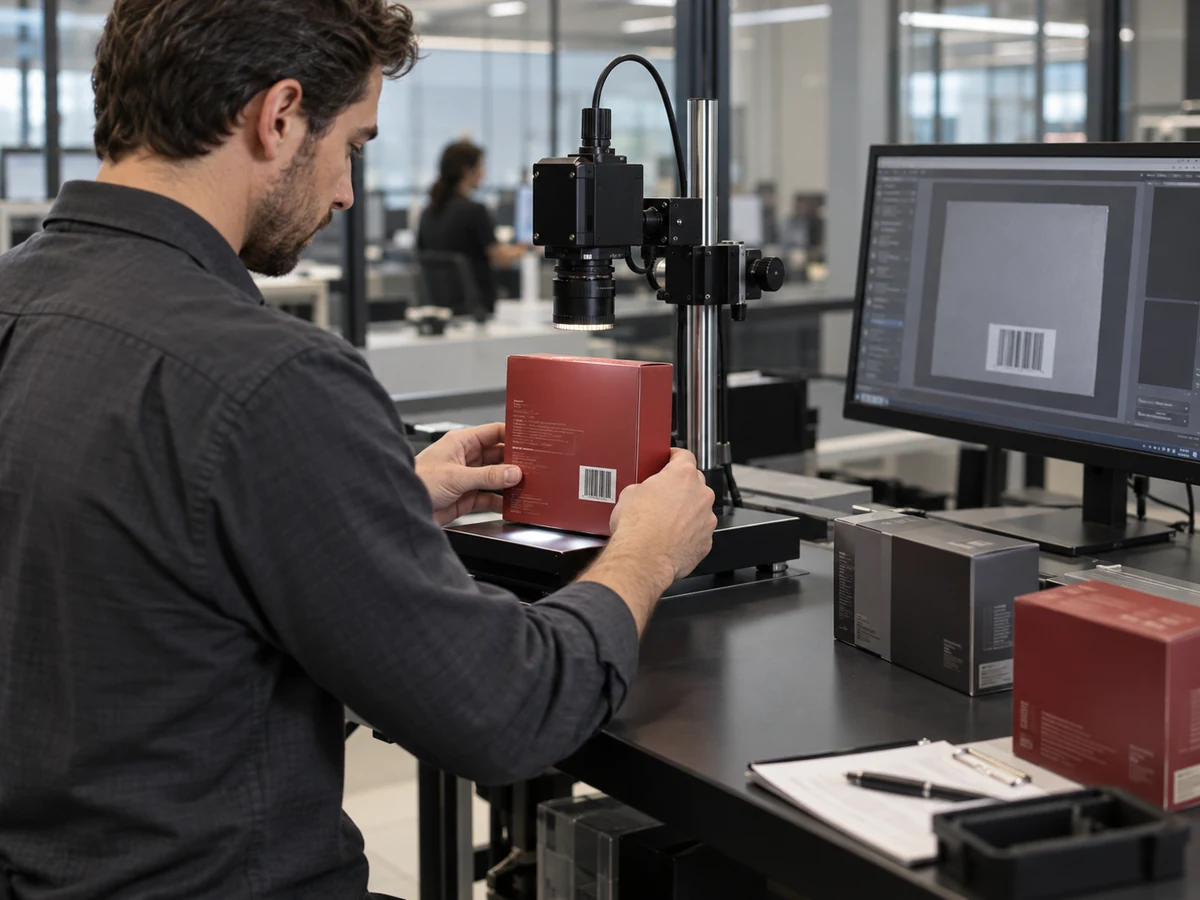
A well-documented complaint gets a faster answer than a vague one. When you find folding carton defects on a sample or a delivery, record the same details each time so the supplier can trace the origin. Keep the physical evidence, note the batch, and compare everything against the approved reference. A useful report covers:
- Approved sample and drawing: the reference the bulk is judged against.
- Defect photos: a wide shot, a close-up, and a measurement against the drawing.
- Batch traceability: lot, run date, and where the units sit in the delivery.
- Incidence: how many units show the defect and whether it is constant or scattered.
Describe what you see without naming the cause you suspect. A report that says “the seam opened on 12 из 50 units from pallet B, photos and lot attached” lets the factory test its own hypotheses. One that says “bad glue” pushes them to defend instead of diagnose. To see how the carton is built before it can go wrong, the guide to how folding cartons are made maps each step where a defect can start.
For a carton structure you can benchmark against, review the custom folding cartons range and keep one approved sample as your reference standard. When you open a claim, send that sample reference and the photo set to PK Paper Box so both sides count the same units.
Часто задаваемые вопросы
What causes cartons to crack along the crease?
Crease cracking can originate from scoring depth, crease rule and matrix selection, applied pressure, grain orientation relative to the fold, влажность доски, or a brittle coating or laminate. The same mark has several possible sources, so confirm the cause against the approved sample, board specification, and converting setup rather than assuming one reason.
Why do carton glue seams open?
An open seam can trace to incorrect glue amount or position, dust or coating on the tab, poor surface compatibility, insufficient compression or setting time, or a seam gap from cutting and folding variation. Record the pattern, incidence, and how the adhesive appears on the failed surfaces so the manufacturer can narrow the cause.
Can lamination cause cracking during folding?
Да. A film or coating that is brittle at the fold radius can split when the crease is formed. It shows as a crack along the fold even when the board itself is sound. Note any finishing on the panel when you report a crease crack, since it may be part of the cause.
Why does a folding carton not stay square?
A carton that stands out of square usually reflects alignment between the cut, the crease, and the glue tab rather than a single fault. A worn or mis-set die, drift on the press, or a seam geometry problem can each contribute. Measure the blank against the drawing to narrow it down.
What causes printing and die-cutting misalignment?
Print misregistration can result from plate or cylinder setup, sheet feeding, substrate movement, or dimensional change during production. Die-cut misalignment occurs later, when the cut and crease positions do not register with the printed artwork. Record whether the artwork, cut line, or crease line is out of position so the supplier can identify the process stage involved.
Are minor cosmetic defects always grounds for rejection?
Not always. A cosmetic variance is judged against the acceptance limit you set for that order, which can differ between a display panel and a hidden interior. Define the limit and reference the approved sample, rather than applying one fixed rule to every defect.
What evidence should buyers provide when reporting defects?
Send the approved sample reference, photos that include a close-up and a measurement, the batch and lot details, and the count of affected units. Describe what you observe and where it falls in the delivery, which lets the factory trace the origin quickly.
A folding carton defect becomes solvable the moment it is described precisely. Separate the functional from the cosmetic, list possible causes without declaring one, and anchor every claim to the approved sample, the drawing, and the batch record.